Customer Journey / Renata PLC / Truck Loading Conveyor & Flexible Roller Conveyor

Truck Loading Conveyor & Flexible Roller Conveyor

Closed Jan 13, 2025 → Feb 20, 2025

Project Overview

The Renata PLC Truck Loading Conveyor & Flexible Roller Conveyor Project was developed to support carton movement and truck loading activities inside the customer’s pharmaceutical facility. The project combines two types of conveyor equipment under MACHLION: a Truck Loading Conveyor and a Flexible Roller Conveyor.

Instead of using one fixed conveyor for every movement, the project uses different conveyor types for different parts of the handling process. The Truck Loading Conveyor supports movement toward the truck loading area, while the Flexible Roller Conveyor provides a movable roller path for cartons inside the warehouse.

Equipment Supplied

The project includes:

  • 2 Sets – MACHLION Truck Loading Conveyor
  • Model: B6-800
  • 2 Sets – MACHLION Flexible Roller Conveyor
  • Model: R-12000
  • Total: 4 Conveyor Sets

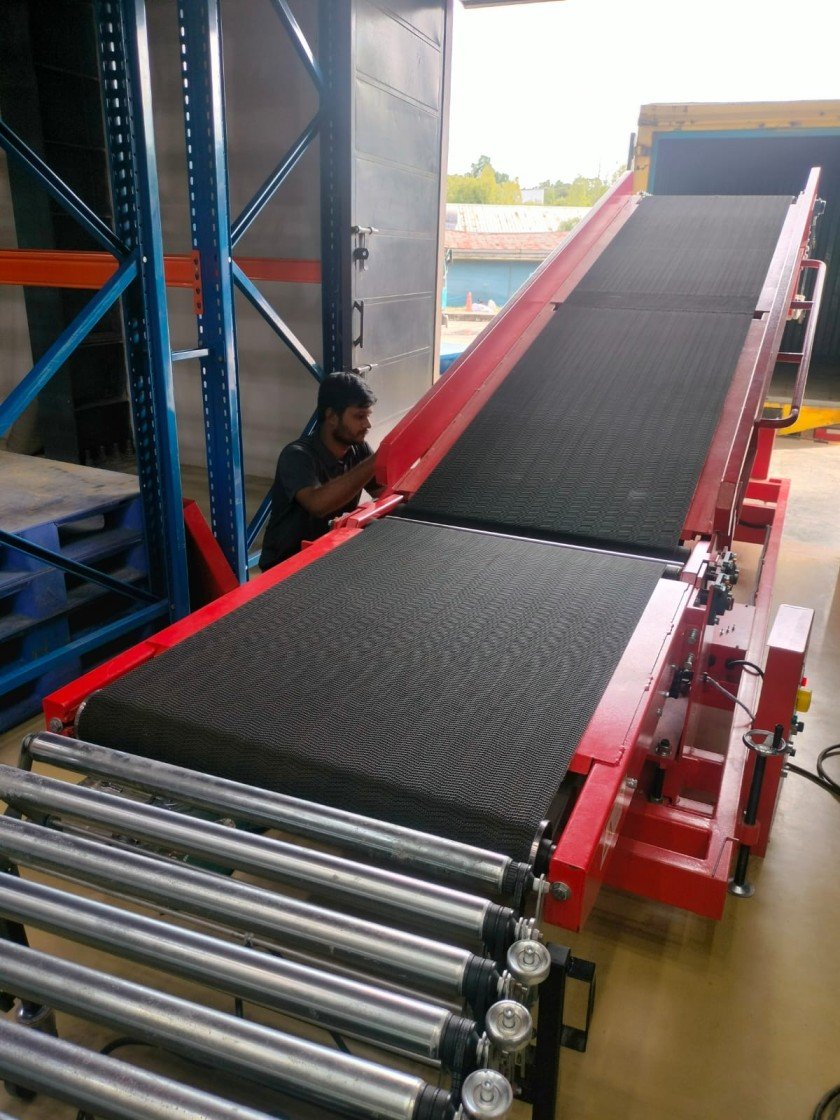
The Truck Loading Conveyor is supplied with an inclined belt section and extension roller section, together with side guards. The Flexible Roller Conveyor is also supplied with side guards.

MACHLION Truck Loading Conveyor – B6-800

The B6-800 Truck Loading Conveyor is the powered conveyor section of the project.

The machine plate confirms the following technical details:

  • Extension Length: 6,000 mm
  • Capacity: 50 kg/meter
  • Run Direction: Bidirectional
  • Power: 4.4 kW
  • Voltage: 3-Phase, 380V / 50Hz
  • Country of Origin: China

The bidirectional running direction allows the conveyor to operate in both directions within its designed working setup. The system combines the inclined belt section with the extension roller section, creating a continuous conveyor arrangement for the truck loading application.

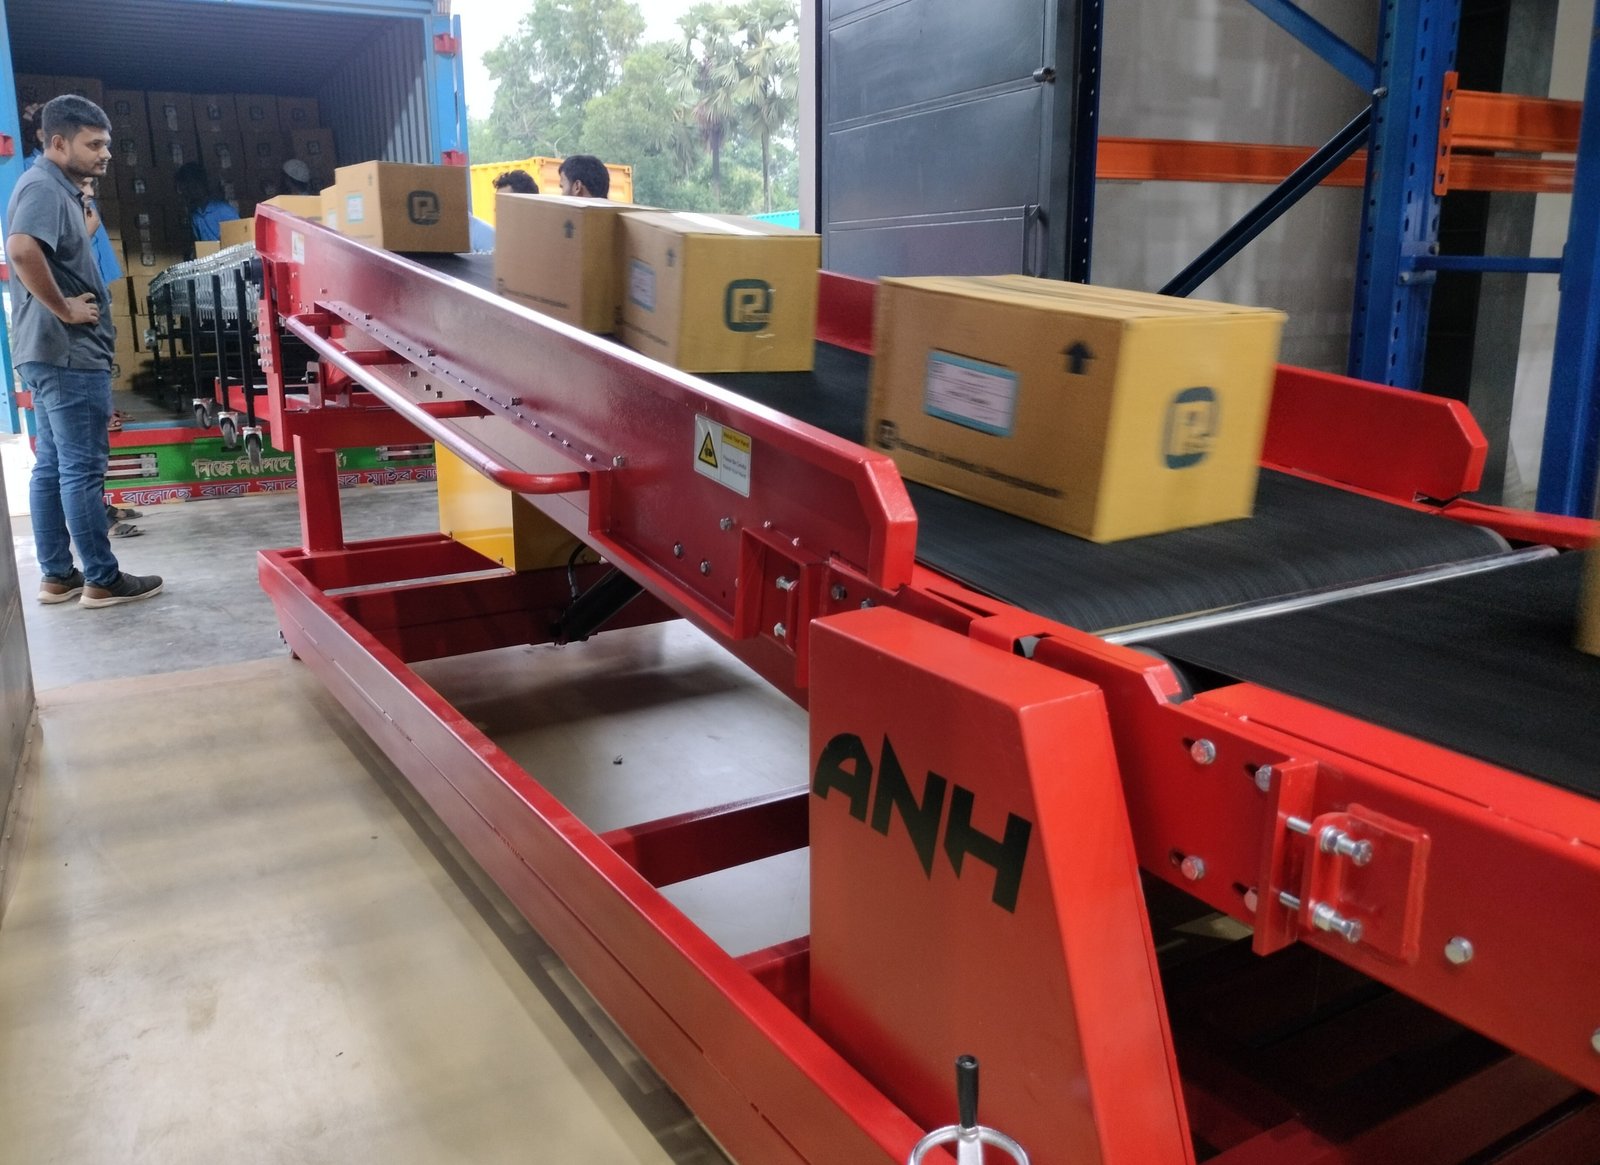
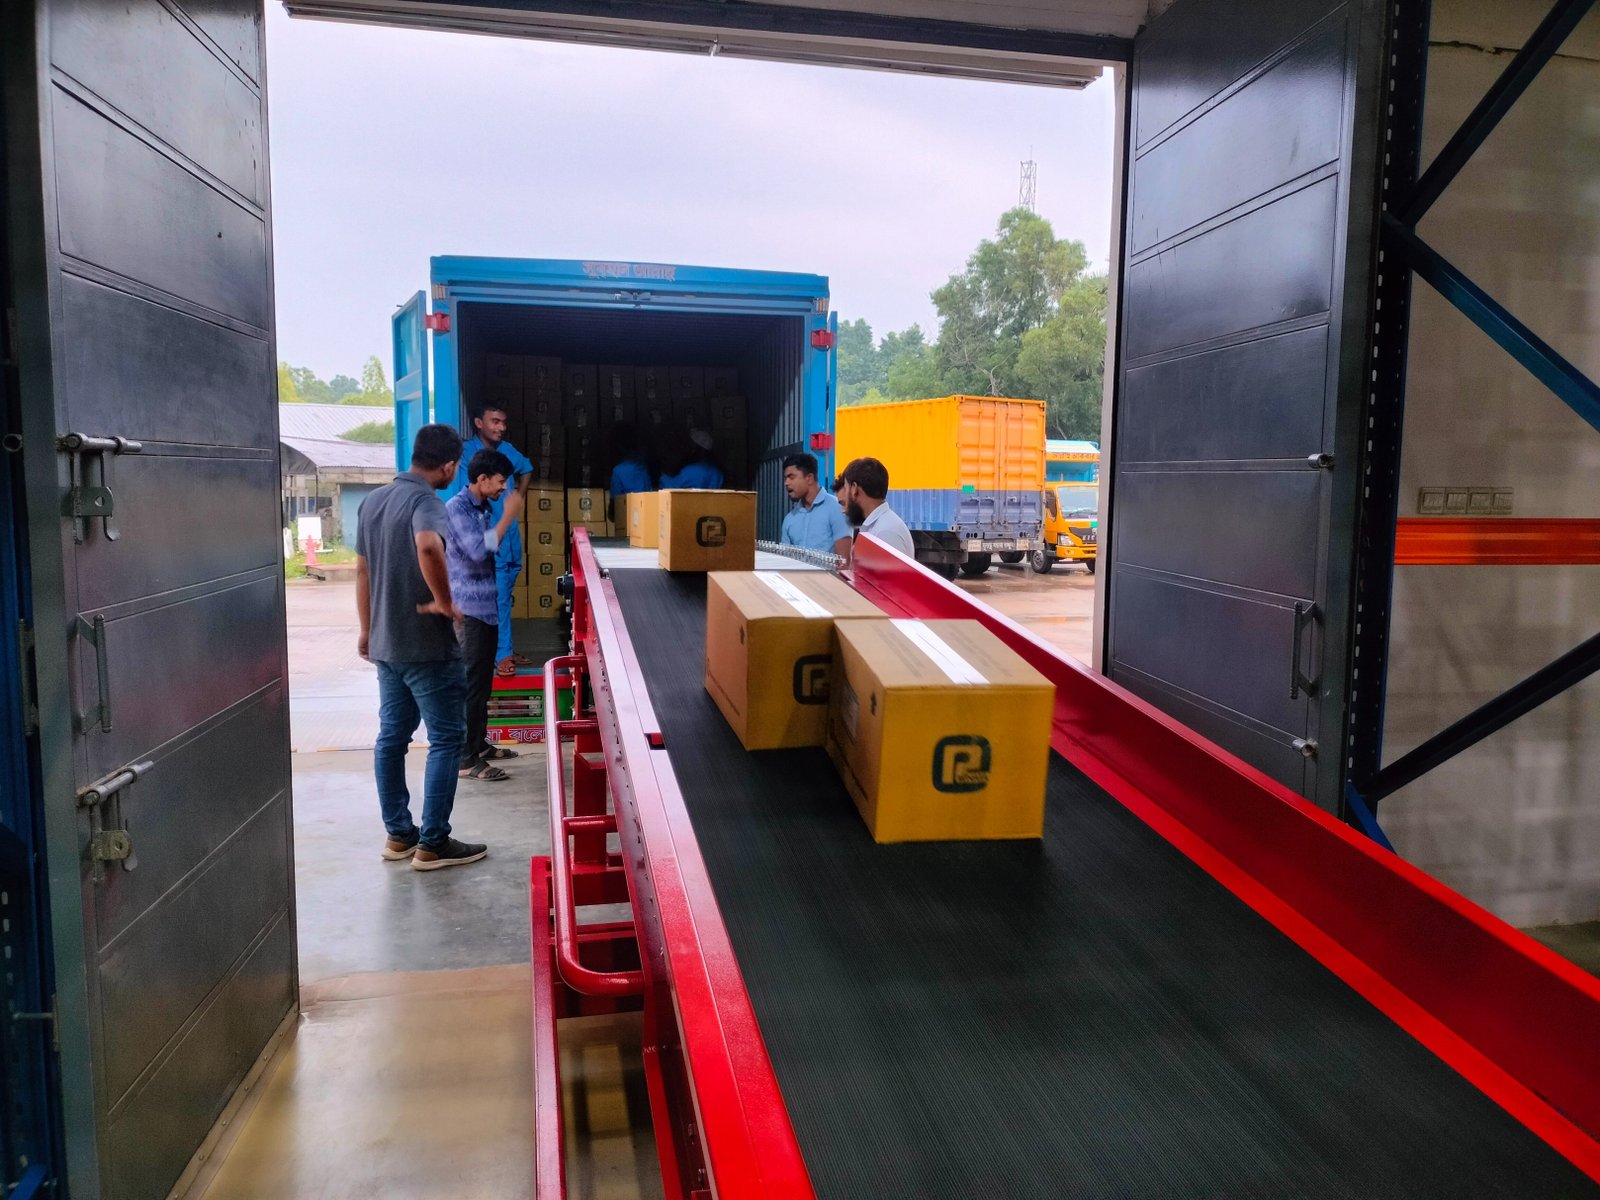
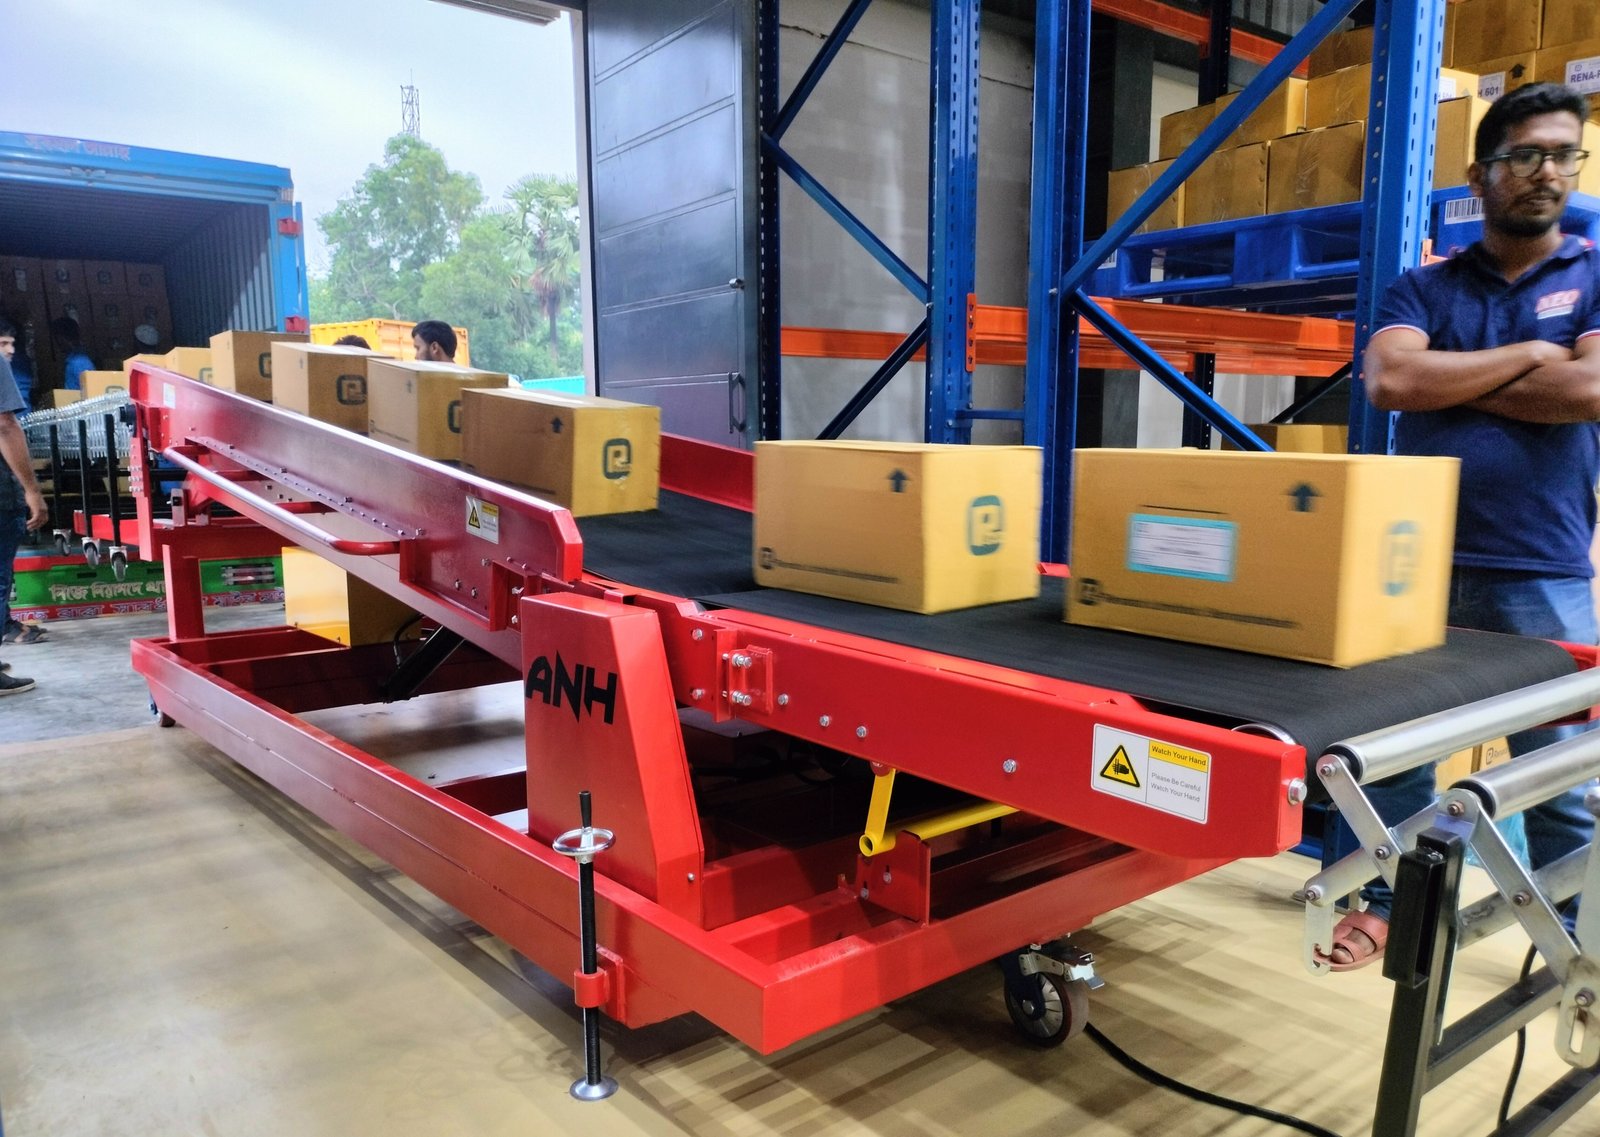
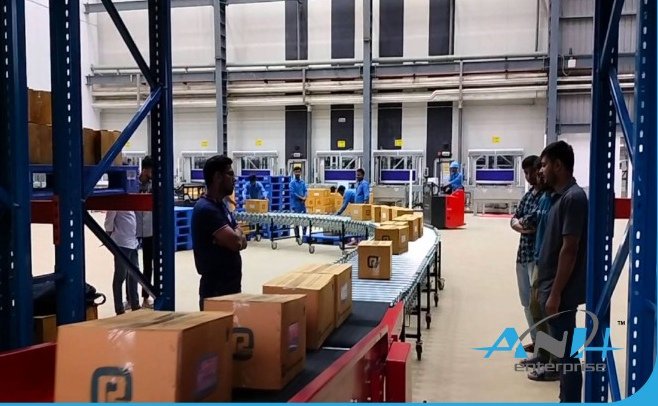
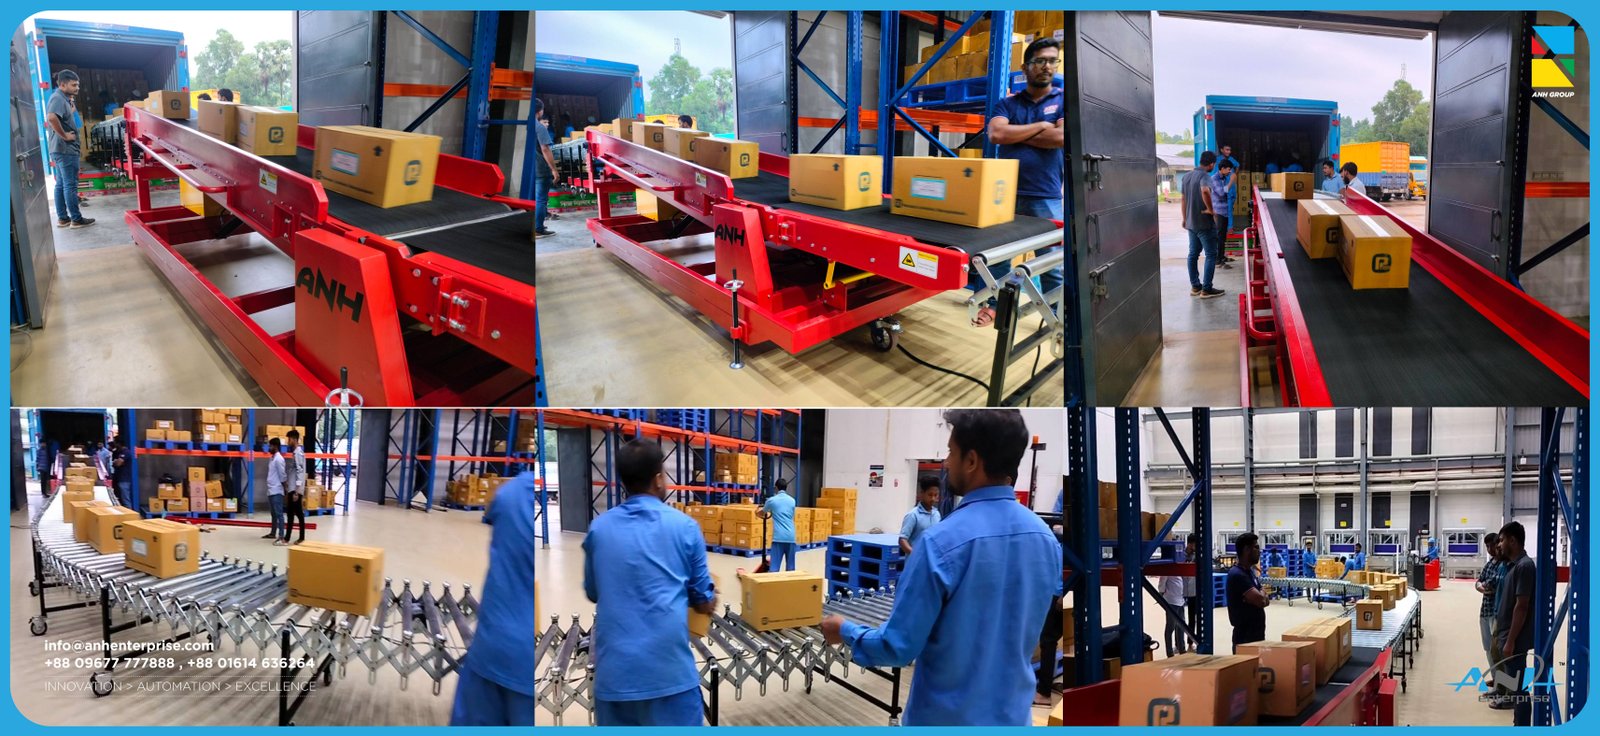
The project photos show cartons moving along the conveyor between the warehouse area and the truck loading point. This gives customers a real view of how the equipment is positioned and used in an actual industrial environment.

MACHLION Flexible Roller Conveyor – R-12000

The second part of the project is the MACHLION R-12000 Flexible Roller Conveyor.

A total of 2 sets were supplied, each with side guards.

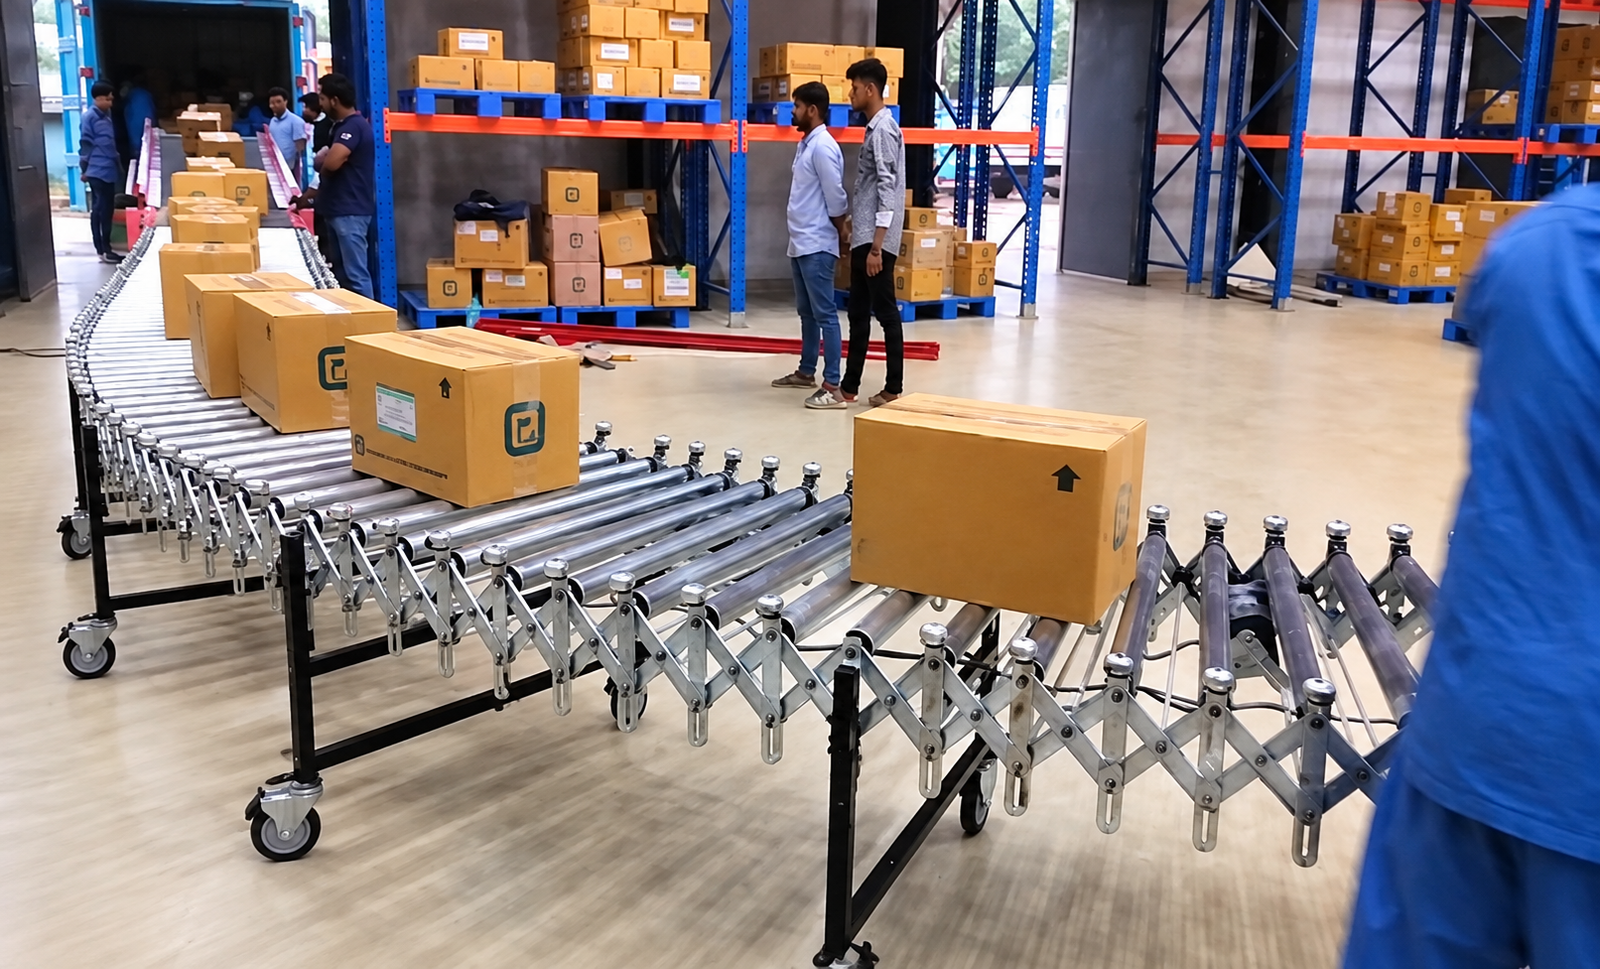
The real project photos show the flexible roller conveyor being used with cartons inside the warehouse. Its expandable roller structure allows the conveyor path to be arranged according to the working area shown in the project.

This makes it a useful part of the overall material movement setup, especially where cartons need to travel between different points inside the warehouse.

A Combined Conveyor Setup

One of the main features of this project is the combination of powered truck loading conveyor equipment and flexible roller conveyor equipment within the same material handling operation.

The Truck Loading Conveyor provides the powered conveyor section for the loading application, while the Flexible Roller Conveyor provides a flexible carton-handling route inside the warehouse.

The project therefore brings together:

  • Powered conveyor movement
  • Flexible roller movement
  • Carton handling
  • Warehouse-to-loading-area movement
  • Side-guard protection on the supplied conveyor configurations
  • Two separate conveyor types for different handling requirements

The project is for a pharmaceutical industry application, as stated in the supplied project document.

Real Project Reference

For companies searching for a truck loading conveyor in Bangladesh, flexible roller conveyor, warehouse conveyor system, carton handling conveyor, or material handling conveyor for pharmaceutical industry, this Renata PLC project provides a real reference of how different conveyor types can work together within one facility.

The project photos are particularly useful because they show the MACHLION conveyor system with actual cartons, warehouse racking, workers, and the truck loading environment. Visitors can understand the scale and arrangement of the equipment without relying only on catalogue images.

Overall, the Renata PLC Truck Loading Conveyor & Flexible Roller Conveyor Project combines 2 MACHLION B6-800 Truck Loading Conveyors and 2 MACHLION R-12000 Flexible Roller Conveyors into one practical conveyor setup for carton movement and truck loading activities.

Project Gallery
Project Videos

What We Solved

For Renata PLC, the main requirement was to create a more practical way to move cartons inside the warehouse and continue that movement toward the truck loading area.

This project was not handled with one fixed conveyor only. Two different conveyor types were used together: the MACHLION Truck Loading Conveyor and the MACHLION Flexible Roller Conveyor. Each one has a different role in the overall carton-handling process.

The result is a conveyor setup that connects internal warehouse movement with truck loading activity in a more organized way.

Moving Cartons Through the Warehouse

Cartons may need to move from one point of the warehouse to another before reaching the loading area. A fixed straight conveyor is not always suitable for every part of that movement, especially where the route needs to change according to the working area.

For this part of the operation, the project uses the MACHLION Flexible Roller Conveyor, Model R-12000.

A total of 2 sets were supplied, and the project document confirms that the conveyors include side guards.

The flexible roller conveyor gives the warehouse a movable conveyor path for cartons. From the real project photos, the conveyor can be seen arranged between the storage area and the loading side, with cartons moving along the rollers.

This makes it useful where the working route is not always limited to one fixed straight line.

For customers looking for a flexible roller conveyor in Bangladesh, warehouse carton conveyor, or expandable roller conveyor for material handling, this project gives a real industrial example of how the system can be used inside a warehouse.

Connecting Warehouse Movement With Truck Loading

The next part of the requirement was the actual loading side.

For this, the project uses the MACHLION Truck Loading Conveyor, Model B6-800.

The project document confirms that the machine includes an inclined belt part and extension roller part with side guard.

The machine plate also confirms that the conveyor has a 6,000 mm extension length, bidirectional running direction, 4.4 kW power, and 50 kg/meter capacity.

The important point is how this supports the loading process.

Instead of cartons reaching the loading area and then depending only on separate manual movement between the warehouse floor and the truck, the conveyor creates a defined path toward the vehicle.

That gives the loading activity a more structured flow.

Two Conveyor Types, One Material Flow

The strongest part of this project is the way the two conveyor types work together.

The Flexible Roller Conveyor supports carton movement inside the warehouse.

The Truck Loading Conveyor continues the movement toward the truck loading point.

So the overall flow becomes easier to understand:

Warehouse / Storage Area → Flexible Roller Conveyor → Truck Loading Conveyor → Truck

This is the main solution created through the project.

Instead of treating warehouse movement and truck loading as two completely separate activities, the conveyor setup gives them a connected material-handling route.

For a pharmaceutical facility handling cartons, this type of arrangement creates a clearer process for moving goods toward dispatch.

Flexible Movement Where a Fixed Conveyor Is Not Ideal

One important advantage of the R-12000 Flexible Roller Conveyor is its flexible structure.

The real project photos show the roller conveyor extended through the warehouse and positioned according to the working area.

This is useful because a warehouse layout includes racks, open floor areas, loading points and people movement. A permanently fixed conveyor path may not suit every section.

The flexible roller conveyor allows the conveyor route to be arranged according to the available working space.

We are not claiming a specific turning radius, conveyor length or adjustable-height range because those values are not included in the supplied document.

What we can clearly say is that the project uses a flexible roller conveyor rather than only a fixed conveyor section, giving the internal carton movement a more adaptable layout.

Supporting Both Loading and Unloading Direction

The Truck Loading Conveyor machine plate states that the run direction is bidirectional.

This is an important practical feature.

A bidirectional conveyor can run in either direction within its intended operating setup. That gives the machine a useful role in a loading-area application where product movement may need to follow more than one direction depending on the work process.

For customers searching for a bidirectional truck loading conveyor, this is a confirmed feature of the MACHLION B6-800 used in the Renata PLC project.

Handling Cartons Along a Defined Conveyor Route

The machine plate gives the Truck Loading Conveyor a rated capacity of 50 kg per meter.

Rather than presenting this only as a technical number, its practical meaning is that the conveyor has a defined load rating for products moving along the conveyor length.

For an industrial customer, this is important because conveyor selection should not be based only on how the machine looks. The product type and load need to match the conveyor’s specified capacity.

In this project, the conveyor is being used with cartons, as shown in the real project photographs.

Keeping Products Within the Conveyor Path

Both conveyor types are supplied with side guards. The Truck Loading Conveyor has side guards on the inclined belt and extension roller sections, while the Flexible Roller Conveyor is also specified with side guards.

The side guards form part of the conveyor configuration and help define the carton travel path along the conveyor.

This is a simple feature, but an important one in a carton-handling setup where the products are moving through different conveyor sections.

A More Organized Loading Area

The project photos show cartons moving from the warehouse area toward a truck through the conveyor system.

Without making unsupported claims about exact time savings or manpower reduction, one clear benefit of this arrangement is that carton movement follows a defined conveyor route instead of relying only on individual carrying between separate points.

That makes the loading area easier to organize around the material flow.

The project therefore supports:

  • internal carton movement
  • movement toward the truck
  • connection between warehouse and loading area
  • flexible routing inside the warehouse
  • powered movement at the truck-loading section
  • bidirectional operation of the B6-800
  • side-guarded conveyor movement

These benefits come directly from the function and configuration of the supplied conveyor system.

Designed for a Pharmaceutical Industry Application

The project document identifies the supplied equipment as brand-new machinery with standard accessories for pharmaceutical industry.

For Renata PLC, this means the conveyor project is part of a pharmaceutical industrial environment where carton movement and dispatch handling are part of the overall facility operation.

For other pharmaceutical companies searching for a pharmaceutical warehouse conveyor in Bangladesh, carton handling conveyor, or truck loading conveyor for pharmaceutical products, this project provides a useful real reference.

Real Project, Real Working Environment

The photographs from the Renata PLC project are especially valuable because they show the conveyor system in an actual warehouse and loading environment.

Visitors can clearly see:

  • cartons moving on the flexible roller conveyor
  • the conveyor route running through the warehouse
  • warehouse racking beside the conveyor
  • workers around the operating area
  • cartons moving toward the truck loading point
  • the Truck Loading Conveyor positioned directly toward the vehicle

This makes the project easier for customers to understand.

Instead of looking only at a product catalogue, they can see how a truck loading conveyor and flexible roller conveyor work together in a real industrial facility.

Why Two Conveyor Types Were Used

The two conveyor types solve different parts of the same handling requirement.

A Flexible Roller Conveyor is useful inside the warehouse because its layout can follow the working area.

A Truck Loading Conveyor is used at the loading side because it provides the powered and extendable conveyor section needed for movement toward the vehicle.

Using both types creates a better connection between:

internal warehouse movement and truck loading movement.

That is the real strength of this project.

A Practical Conveyor Setup for Carton Handling

The project includes:

  • 2 sets of MACHLION B6-800 Truck Loading Conveyor
  • 2 sets of MACHLION R-12000 Flexible Roller Conveyor

But the value of the project is not simply the number of machines.

The value comes from how the equipment is arranged to support the carton flow.

The Flexible Roller Conveyor provides the adaptable warehouse-side route.

The Truck Loading Conveyor provides the powered connection toward the truck.

Together, they create one continuous material-handling approach for carton movement and loading.

What Makes This Project Different

The key USP of the Renata PLC Truck Loading Conveyor & Flexible Roller Conveyor Project is the combined conveyor approach.

Instead of using only a truck loading conveyor or only a flexible roller conveyor, the project uses both types in the same handling process.

This gives the customer:

  • flexibility inside the warehouse
  • a dedicated conveyor for the loading area
  • a clear route for carton movement
  • bidirectional truck conveyor operation
  • side guards on the supplied conveyor configurations
  • separate conveyor types matched to different parts of the workflow

For industrial customers, this is much more useful than trying to make one conveyor type cover every part of the operation.

The Solution in Simple Terms

Renata PLC needed cartons to move through the warehouse and continue toward the truck loading point.

The solution was to divide that movement into two practical parts.

The MACHLION Flexible Roller Conveyor handles the flexible internal warehouse route.

The MACHLION Truck Loading Conveyor handles the powered movement toward the truck, with a 6,000 mm extension length, bidirectional operation and 50 kg/meter capacity.

Together, the two systems create a clear conveyor path from the warehouse area toward vehicle loading.

That is what this project solved: a connected and practical carton-handling route for warehouse movement and truck loading using the right conveyor type at each stage.

For customers searching for a truck loading conveyor in Bangladesh, flexible roller conveyor in Bangladesh, warehouse conveyor system, carton handling conveyor, expandable roller conveyor, pharmaceutical warehouse conveyor, loading unloading conveyor, or industrial material handling conveyor, the Renata PLC project provides a real example of a combined MACHLION conveyor solution.